-
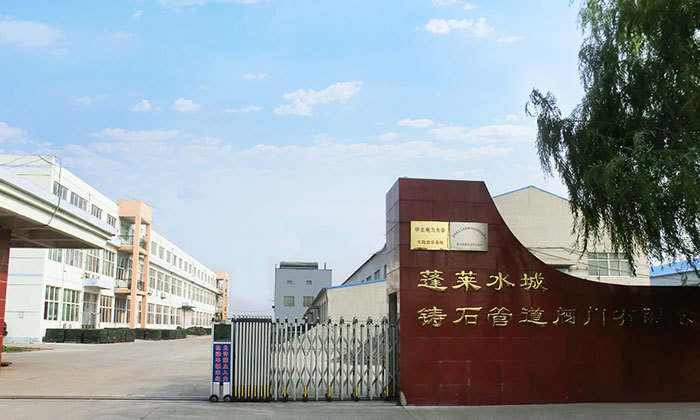
About UsSpecializing in the production and sales of wear-resistant materials such as cast basalt products, the company has obtained over 20 invention patents and utility model patents, and was awarded the "Shandong Star Enterprise of China Patent" title. The company has a history of over 20 years, and currently owns a single basalt cast basalt production line with a production capacity of 15000 tons/year, and mechanical processing equipment with an annual output of 5000 wear-resistant valves and 20000 clamp-type flexible pipe joints.
-
Cast BasaltCast basalt products include cast basalt pipes, cast basalt tiles, cast basalt powder, cast basalt lined steel pipes, etc., mainly used in industries such as electric power, metallurgy, mining, coal, building materials, and chemical.

-
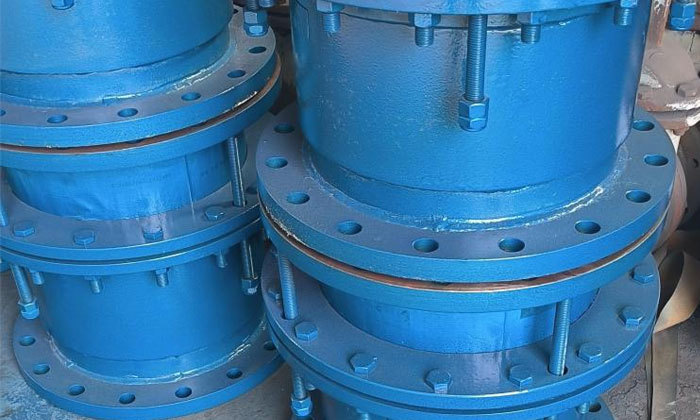
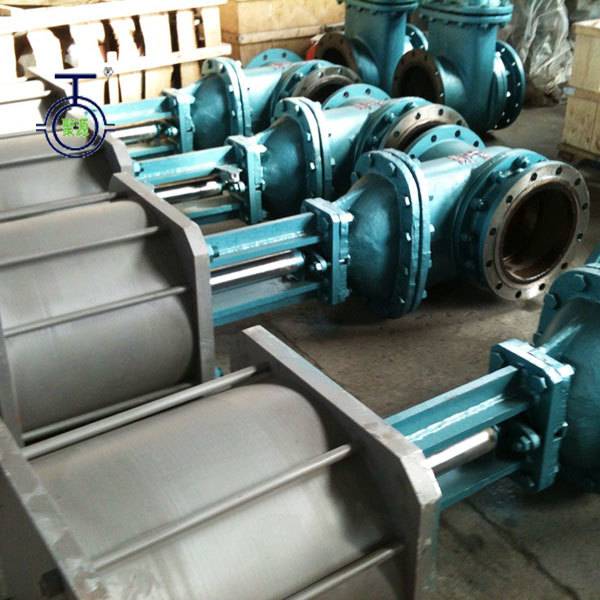
ValveCast basalt ball valves are durable, have a long service life, low fluid resistance, reliable sealing, wear and corrosion resistance, and the sealing surfaces of the ball and valve seat are always isolated from the medium during the fully open and fully closed processes of the valve, so that the medium passing through the valve at high speed will not erode the sealing surface.
-
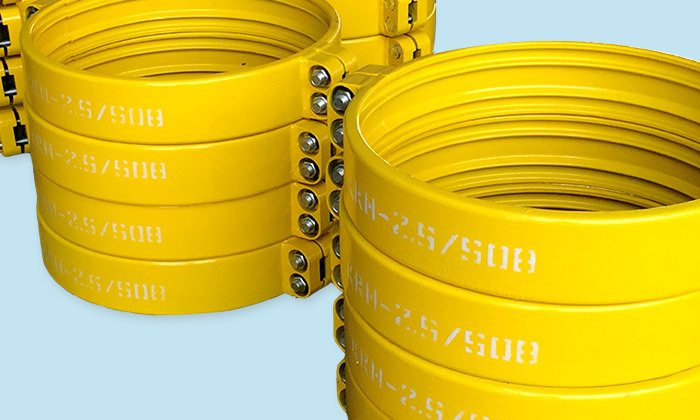
Pipe FittingClamp-type flexible pipe joints are used to connect pipes. KRH and KRJ series rolled clamp-type flexible pipe joints are patented products of our factory. They can effectively compensate for thermal expansion and contraction caused by temperature changes in the pipeline system, and can also compensate for angular changes caused by pipeline foundation settlement. They are high-pressure resistant, easy to install, and have a much better price-performance ratio than flange connections.
-
BLOGSince its establishment in 1986, the company has cumulatively produced: over 1600 kilometers of cast basalt lined steel pipes; over 260000 sets of flexible pipe joints; over 18000 valves of various types. Its products cover all provinces nationwide and are exported to countries such as South Korea, the United States, Serbia, South Africa, Zimbabwe, Japan, India, Vietnam, Russia, Poland, Ukraine, Kazakhstan, and Australia.
Understanding Non-Return Valves for Ash Pipelines in Industrial Applications
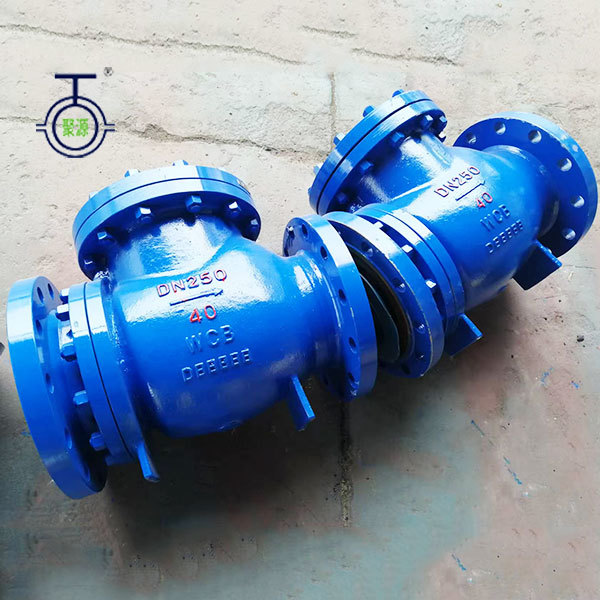
Non-return valves, also known as check valves, are crucial components in ash pipelines used in a variety of industrial applications, particularly in the management of particulate waste produced during combustion processes. The primary function of these valves is to prevent the backflow of ash and other materials, ensuring a smooth and efficient flow through the pipeline system. By doing so, they h
In ash handling systems, non-return valves are typically installed to manage the flow of ash from boilers or combustion chambers to disposal areas or processing units. Their design is tailored to cope with abrasive materials, high temperatures, and varying pressure conditions. This makes them indispensable in systems dealing with fly ash, bottom ash, or other combustion residues.
One of the key technical features of non-return valves for ash pipelines is their construction material. These valves are often made from robust materials such as cast iron, stainless steel, or specially engineered composites to withstand harsh conditions. Their internal mechanisms are designed to respond quickly to changes in pressure, ensuring that the valve opens and closes effectively to prevent backflow while minimizing wear and tear from abrasive particles.
Installation and maintenance of non-return valves in ash handling systems require careful consideration. Proper alignment and sealing are crucial to prevent leaks and ensure the longevity of the valve. Additionally, routine inspections and maintenance are necessary to address any wear that may occur over time due to the abrasive nature of ash. This proactive approach helps avoid unexpected downtimes and enhances the overall efficiency of the ash handling system.
Another important aspect to consider is the valve sizing and selection. The correct sizing is essential to ensure optimal flow rates and pressure differentials. Engineers and technicians must evaluate the specific requirements of their ash pipeline systems, including flow velocity, particulate size, and system pressure, to select the most suitable non-return valve.
In conclusion, non-return valves play a vital role in the efficient operation of ash pipelines within the industrial equipment sector, particularly in casting and heat treatment applications. Their ability to prevent backflow, combined with robust construction and proper maintenance, ensures reliable performance in managing ash. Understanding the technical details and best practices surrounding these valves is essential for professionals seeking to optimize their ash handling processes.
Recommended

Maximizing Efficiency: A Comprehensive Guide to NPZ Wear-resistant Slurry Gate Valves Performance

Supplier of wear-resistant material solutions, specializing in cast basalt products
Many years of focus on the production and sales of high-quality wear-resistant materials, mainly used in power, metallurgy, mining, coal, building materials, chemical, and other industries.
Leave your contact information to get the latest product discount information

Mobile Website
Contact Us
Phone: +86-535-5632189 / 5666528 / 5637763
Fax: +86-535-5666528 / 5642975
Email: z.minhui@plsczsgdfm.com
Address: No. 6 Zhenxing, Liujiagou Town, Penglai District, Yantai City, Shandong Province


